Choosing the right coating equipment can shape product quality, production speed, and long-term operating costs. Global buyers often compare machines by appearance, price, and advertised capacity. That approach can be misleading. The most suitable types of coating machine depend on material viscosity, coating width, target thickness, drying conditions, and production volume.
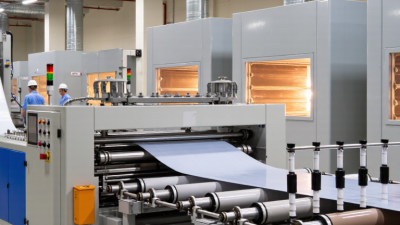
In practical factory evaluations, a roll coater may provide stable coverage for films, paper, or metal sheets. A spray coater can reach uneven surfaces, but it may require stronger ventilation and careful overspray control. Slot-die and curtain coating systems can deliver precise layers, especially in controlled continuous production. Dip coating remains useful for complex shapes, although liquid management can become demanding. Small details matter. A clean doctor blade, steady web tension, and accurate temperature control often influence results more than a polished brochure.
This guide presents seven practical tips for comparing coating machines across international markets. It considers application fit, machine configuration, automation, maintenance access, energy use, and supplier support. Technical drawings, sample tests, spare-parts lists, and documented performance data deserve close attention. Certifications and operating instructions should also match the buyer’s region and workplace requirements. No machine is perfect. Some systems appear efficient during demonstrations but perform differently with real materials, changing humidity, or frequent product adjustments. Buyers should request trial coating, inspect the finished layer under consistent lighting, and record measurable results. A thoughtful decision may take longer, but it reduces costly surprises after installation.
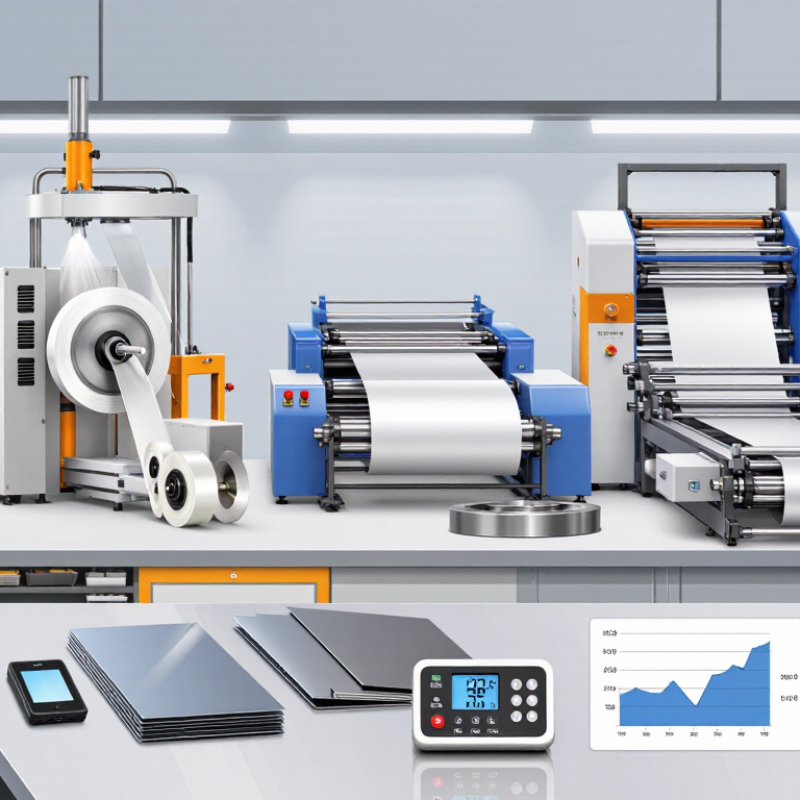
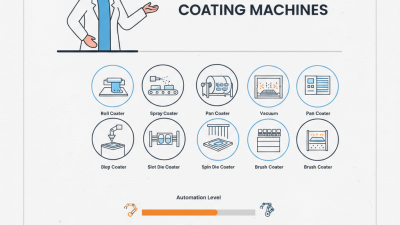
Understanding coating machines starts with the application, not the machine name. Roll-to-roll systems suit films, foils, and battery electrodes. Slot-die coating delivers controlled layers with limited material waste. Spray systems handle complex surfaces, while dip coating reaches hidden edges. Curtain coating works well for flat panels and high-volume lines. Choose a machine that matches viscosity, width, speed, and substrate sensitivity. Check cleaning access carefully. Downtime often begins there.
According to the IEA’s Global EV Outlook 2024, battery demand exceeded 750 GWh in 2023, rising about 40%. This growth increases demand for precise electrode-coating equipment.
Industrial applications require measurable controls. Review coating thickness, drying temperature, line tension, solvent recovery, and transfer efficiency. Powder systems may reduce solvent use, but they still require reliable curing and filtration.
The European Commission’s Best Available Techniques reference documents emphasize emission control and energy efficiency in surface treatment. MarketsandMarkets estimated the global coating equipment market at roughly 20 billion dollars in 2023, with continued growth expected through 2028. Treat forecasts cautiously. They can hide regional differences.
During factory evaluations, buyers should request trial data using their actual material. Laboratory performance may not survive dust, vibration, or shift changes. Ask for calibration records, operator training plans, spare-part availability, and safety documentation. A cheaper machine can become expensive when cleaning takes longer than production.
Coating machines differ by process, material, and finished product. A spray booth applies liquid paint, while a powder line uses electrostatic charging and oven curing. Roll-to-roll systems coat films, foils, and flexible laminates with steady web tension. MarketsandMarkets estimates the global coating equipment market could grow from USD 18.9 billion in 2023 to USD 25.7 billion by 2028, at a 6.3% CAGR.
Tip 1: Define the process first. Choose spraying, dipping, curtain coating, or slot-die coating according to viscosity and surface shape.
Tip 2: Check the material chemistry. Water-based coatings need different pumps and drying controls than solvent-based or powder materials.
Tip 3: Match the machine to the product. Metal parts may require corrosion protection, while packaging films need precise, thin layers.
Tip 4: Measure the target thickness. ASTM D7091 provides guidance for dry-film thickness measurement on nonmagnetic coatings.
Tip 5: Review curing conditions carefully. Infrared, hot-air, and ultraviolet systems create different heat profiles.
Tip 6: Compare production scale, not only purchase price. A compact batch coater may suit varied orders, but a continuous line can reduce labor per unit.
Tip 7: Ask for test panels using your real substrate. Laboratory results can look perfect. Factory results may disagree.
ISO 12944 helps buyers evaluate protective coating systems for steel, but it does not replace site-specific testing. My own caution is simple: automation reduces variation, yet poor surface preparation still produces weak adhesion and costly rework.
Tip 1: Match the machine with your substrate. Roll-to-roll coaters suit films, foils, and continuous webs. Sheet-fed systems work better for rigid panels or cut parts.
Tip 2: Check coating thickness before chasing speed. Slot-die machines provide controlled layers for accurate, repeatable production. However, they need stable material flow and careful gap adjustment.
Tip 3: Consider liquid behavior. Spray systems handle uneven surfaces and complex shapes. Curtain coaters perform well on wide, flat panels. High-viscosity coatings may require heated tanks or stronger pumping systems.
Tip 4: Compare output with drying capacity. A fast coater can create a bottleneck near the oven. I have seen production plans fail because curing space was underestimated.
Tip 5: Review changeover time. Frequent color or material changes favor accessible designs and simple cleaning routes. Less downtime matters.
Tip 6: Ask for trial coating data. Test edge quality, surface smoothness, adhesion, and waste rate using your actual material. Supplier demonstrations can look perfect, but factory conditions are rarely identical.
Tip 7: Inspect control and safety functions. Check tension control, temperature monitoring, ventilation, and emergency access. These details support consistent operation and safer maintenance.
A machine with the highest advertised speed may not deliver the lowest cost. Energy use, operator skill, rejected parts, and spare components also affect performance. Leave room for adjustment; real materials can behave differently between batches.
7 Tips on Types of Coating Machines for Global Buyers
Evaluating Automation, Capacity, Precision, and Maintenance Needs
Choosing a coating machine starts with the material, not the machine brochure. Roll-to-roll systems suit continuous films, while spray, dip, curtain, slot-die, and knife coaters serve different surfaces. Ask how much operator intervention your process can tolerate. Servo drives, recipe storage, automatic tension control, and inline inspection can reduce variation. However, excessive automation may increase training and repair demands.
Capacity needs careful measurement. Check usable coating width, line speed, batch size, drying length, and daily operating hours. A fast coater is not always productive if the dryer cannot remove moisture evenly. Precision depends on viscosity control, surface tension, metering accuracy, and substrate stability. Request trial data with your actual material. Small edge defects may appear only after several hours.
Maintenance often decides long-term value. Look for tool-free access, washable components, clear lubrication points, and commonly available wear parts. Ask how long cleaning and changeovers take. I have seen impressive equipment lose production because a filter required difficult removal. That detail was missed.
Global buyers should also verify power requirements, environmental conditions, operator language, spare-part logistics, and local service capability. Humid workshops may need better corrosion protection and climate control. Keep records of calibration and coating weight. They reveal drift early. No specification is perfect. A practical pilot run can expose assumptions that a polished quotation hides.
| Tip & Machine Type | Typical Applications | Typical Working Capacity | Coating Precision | Automation Potential | Maintenance Needs | Best Buying Consideration |
|---|---|---|---|---|---|---|
| 1 Roll-to-Roll Gravure Coater | Flexible packaging films, decorative laminates, labels, aluminum foil, and printed electronics. | Web widths commonly range from approximately 300 to 2,000 mm; line speeds may reach about 50 to 300 m/min, depending on coating chemistry and drying requirements. | High. Coat-weight consistency is often controlled within approximately ±5% under stable process conditions. | High. Automatic tension control, register control, viscosity monitoring, splice handling, and recipe management are available. | Medium to high. Requires regular cleaning of engraved cylinders, doctor blades, pumps, filters, rollers, and solvent-handling components. | Check web-tension stability, cylinder changeover time, solvent recovery, drying-zone capacity, and operator safety systems. |
| 2 Slot-Die Coater | Battery electrodes, separator films, optical films, adhesive tapes, specialty coatings, and laboratory-to-production scale products. | Common working widths range from approximately 100 to 2,000 mm; coating speeds may range from less than 1 m/min in development work to over 100 m/min in selected production processes. | Very high. It can deliver uniform, pre-metered coating with low edge variation when viscosity, gap, and web stability are controlled. | High. Closed-loop pump control, automatic gap adjustment, inline inspection, and multi-layer coating options are available. | Medium. The die lips, shims, manifolds, filters, and fluid lines must be cleaned carefully to prevent streaks and blockages. | Prioritize coating-window testing, pump pulsation control, die-cleaning access, material compatibility, and minimum practical batch size. |
| 3 Spray Coating Machine | Metal parts, automotive components, furniture, plastics, appliances, and irregular three-dimensional surfaces. | Suitable for small components through large parts; automated booths commonly use reciprocators or robots with conveyor-based throughput. | Medium to high. Film uniformity depends on atomization, spray distance, gun movement, viscosity, and overspray control. | High when equipped with robots, automatic gun cleaning, color-change systems, and conveyor tracking; manual versions offer lower automation. | Medium to high. Spray guns, nozzles, hoses, filters, booth surfaces, pumps, and exhaust systems require frequent cleaning and inspection. | Evaluate transfer efficiency, booth airflow, ventilation, explosion protection, color-change time, and compliance with local emissions rules. |
| 4 Dip Coating Machine | Fasteners, wire products, metal components, printed circuit assemblies, corrosion protection, and laboratory specimens. | Batch or continuous systems can handle individual parts, baskets, or long profiles; cycle time is generally governed by immersion and withdrawal speed. | Medium. Thickness is strongly affected by withdrawal speed, liquid viscosity, drainage, surface tension, and part geometry. | Medium to high. Hoists, indexing conveyors, automatic immersion cycles, agitation, and bath-level control can be integrated. | Low to medium. Main tasks include bath filtration, concentration checks, sludge removal, tank cleaning, and hanger maintenance. | Confirm tank volume, load weight, drainage space, bath-life management, chemical compatibility, and wastewater treatment requirements. |
| 5 Curtain Coater | Flat wood panels, furniture boards, flooring, glass, composite panels, and high-volume decorative finishing. | Typically used for continuous flat substrates; working widths often range from approximately 600 to 1,600 mm, with line speeds commonly around 10 to 80 m/min. | High on flat surfaces. Uniformity depends on curtain stability, substrate flatness, liquid flow rate, and conveyor speed. | High. Automatic flow control, conveyor synchronization, viscosity monitoring, and return-tank management are commonly used. | Medium. The curtain head, recirculation tank, filters, pumps, and conveyor must be cleaned to avoid surface defects. | Verify the minimum coating flow rate, substrate flatness tolerance, recovery ratio, edge-loss control, and cleaning/changeover procedure. |
| 6 Powder Coating Line | Steel furniture, appliances, architectural aluminum, automotive parts, electrical enclosures, and general metal fabrication. | Conveyor widths commonly range from approximately 500 to 2,000 mm; throughput depends on part size, hanging density, oven length, and curing temperature. | High after curing when grounding, powder delivery, film thickness, and oven temperature are properly controlled. | High. Automatic guns, reciprocators, booth recovery, color management, conveyor controls, and oven monitoring are available. | Medium. Booth filters, recovery equipment, spray guns, powder pumps, oven burners, and conveyor hooks require scheduled service. | Compare oven energy consumption, powder recovery efficiency, color-change time, grounding quality, booth design, and available floor space. |
| 7 Vacuum Coating System | Decorative metal finishes, optical components, electronics, wear-resistant tools, plastics, and barrier films. | Batch chambers commonly accommodate parts from small components to large panels; batch time may range from roughly 20 minutes to several hours depending on pretreatment and film stack. | Very high. Thickness and composition can be tightly controlled using monitored vacuum, gas flow, power, and substrate movement. | Very high. PLC recipes, automated pumping sequences, plasma pretreatment, process monitoring, and data logging are standard options. | High. Vacuum seals, pumps, targets or evaporation sources, fixtures, chamber shields, cooling systems, and sensors need periodic service. | Assess chamber size, pump-down time, substrate loading method, process repeatability, utility requirements, preventive-maintenance cost, and technical support availability. |
Choosing a coating machine for global purchasing requires more than comparing output speed. The coating method must match the substrate, liquid viscosity, production width, and drying behavior. Roll-to-roll systems suit continuous films and web materials. Spray units handle uneven surfaces. Dip coating can cover complex shapes, but it may waste more material. Slot-die systems offer precise layers when fluid control is stable.
Ask suppliers for measurable evidence. Request coating thickness tolerances, line-speed records, energy data, and sample results from similar materials. A factory acceptance test with your actual substrate can reveal defects that brochures hide.
Small details matter. Check nozzle access, cleaning time, spare-part availability, and operator training. A machine that runs well but takes hours to clean may reduce real productivity.
Compliance needs a document trail. Review electrical safety, electromagnetic compatibility, pressure components, guarding, and emergency-stop design for the destination market. Confirm whether local certification, language labels, installation permits, or environmental controls apply. If coatings release vapors, inspect ventilation and emissions requirements before shipment.
Ask for manuals, wiring diagrams, risk assessments, material declarations, and serial-number records. Do not assume one certificate covers every country. It usually does not.
I have seen purchasing teams focus on machine price and overlook customs documents, causing avoidable delays. That mistake is easy to repeat. A local compliance specialist should verify the final configuration, especially after custom modifications.
This site uses cookies. By continuing to browse the site, you are agreeing to our use of cookies.
OKLearn moreWe may request cookies to be set on your device. We use cookies to let us know when you visit our websites, how you interact with us, to enrich your user experience, and to customize your relationship with our website.
Click on the different category headings to find out more. You can also change some of your preferences. Note that blocking some types of cookies may impact your experience on our websites and the services we are able to offer.
These cookies are strictly necessary to provide you with services available through our website and to use some of its features.
Because these cookies are strictly necessary to deliver the website, refusing them will have impact how our site functions. You always can block or delete cookies by changing your browser settings and force blocking all cookies on this website. But this will always prompt you to accept/refuse cookies when revisiting our site.
We fully respect if you want to refuse cookies but to avoid asking you again and again kindly allow us to store a cookie for that. You are free to opt out any time or opt in for other cookies to get a better experience. If you refuse cookies we will remove all set cookies in our domain.
We provide you with a list of stored cookies on your computer in our domain so you can check what we stored. Due to security reasons we are not able to show or modify cookies from other domains. You can check these in your browser security settings.
We also use different external services like Google Webfonts, Google Maps, and external Video providers. Since these providers may collect personal data like your IP address we allow you to block them here. Please be aware that this might heavily reduce the functionality and appearance of our site. Changes will take effect once you reload the page.
Google Webfont Settings:
Google Map Settings:
Google reCaptcha Settings:
Vimeo and Youtube video embeds: