China’s 200*1800mm Graphite Electrode market serves steelmakers and foundries that need consistent electrode dimensions, machining, and performance. The World Steel Association reported 1,882.6 million tonnes of global crude steel production in 2024. Its production statistics also show that electric arc furnaces remain a substantial steelmaking route, where graphite electrodes conduct current and withstand intense heat. That industrial context makes supplier evaluation more than a price comparison.
For buyers, the 200*1800mm Graphite Electrode specification is a starting point, not a full purchasing decision. Diameter and length must match the furnace setup, while bulk density, resistivity, flexural strength, and nipple fit affect operating results. A mill certificate can help verify batch properties. It cannot replace checks on packaging, dimensional tolerances, production capacity, and delivery consistency. Small details matter.
This guide examines leading Chinese manufacturers through practical criteria rather than an unsupported ranking. It considers product documentation, export experience, quality-control procedures, and the ability to supply the requested size. Industry reports provide useful market context, but they do not independently verify any company’s claims. Buyers should request current test reports and confirm specifications directly with each manufacturer. A careful comparison may take longer. That is often worthwhile. No supplier is automatically the right choice, and published product pages may leave important questions unanswered.
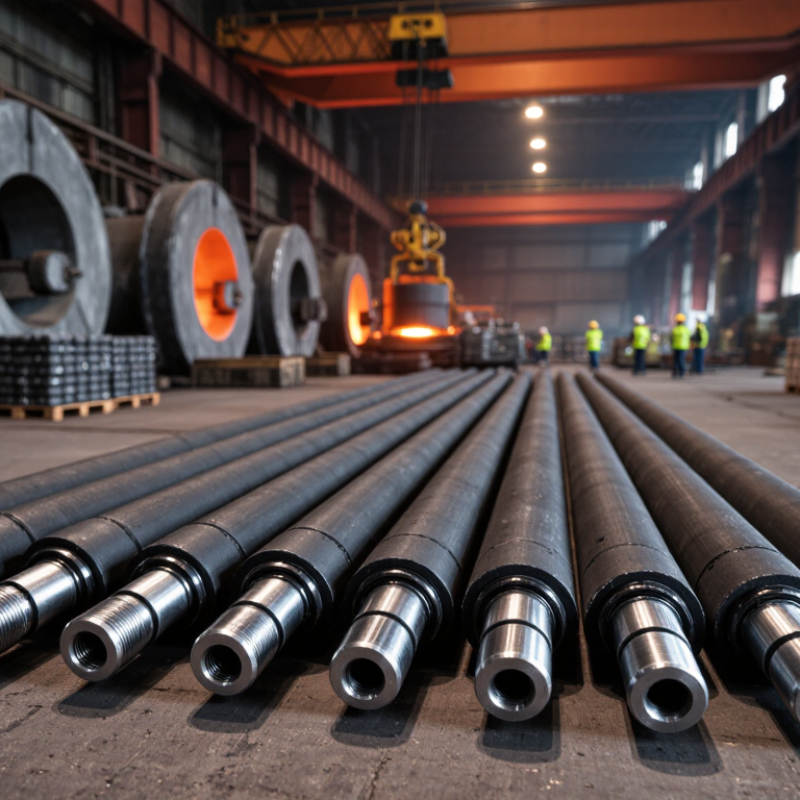
A 200 mm × 1,800 mm graphite electrode designation usually means nominal diameter by overall length. It does not describe the usable length after installation. The nipple joint, machining, and operating losses all matter. A 200 mm electrode can fit a compact furnace setup, but the dimensions alone do not confirm suitability.
Grade is a separate choice. RP, HP, and UHP grades differ in electrical and mechanical properties, including resistivity and flexural strength. Ask for test values and tolerances, not just a grade label. EN 60239:2005 provides dimensional designations for electric-arc-furnace electrodes; purchase specifications should also state the applicable tolerances and connection details. That sounds simple. It is not. World Steel Association’s World Steel in Figures 2024 reports that electric-arc furnaces produced about 28.5% of global crude steel in 2023, making electrode performance relevant across a substantial part of steelmaking. Still, that industry share cannot determine the right grade for one furnace. Check the furnace current, duty cycle, and electrode consumption records. A neat size description can hide important gaps.
For a 200 × 1800 mm graphite electrode, grade selection should follow furnace current, operating conditions, and verified test data. RP, HP, and UHP are not interchangeable labels. Resistivity generally decreases as grade rises, supporting greater current capacity with lower electrical losses. Check whether the supplier reports longitudinal or transverse resistivity, and confirm the test method. Small differences matter. A copied specification without test conditions is not enough.
Bulk density and flexural strength add useful context. RP typically sits lower on both measures, while HP and UHP usually offer denser material and greater resistance to bending. This can matter during lifting, nipple tightening, and furnace operation. But grade alone cannot predict service life. That comparison can be misleading. Ask for actual batch results, dimensional tolerances, and inspection records for the stated 200 mm diameter and 1800 mm length. Compare values on the same units and test basis; density readings, for example, should not be mixed with apparent porosity data. A careful review may reveal variation between batches, so a single attractive number deserves a second look.
| Comparison item | RP grade | HP grade | UHP grade |
|---|---|---|---|
| Nominal electrode size | 200 mm diameter × 1,800 mm length | 200 mm diameter × 1,800 mm length | 200 mm diameter × 1,800 mm length |
| Electrical resistivity | ≤ 9.0 μΩ·m | ≤ 6.5 μΩ·m | ≤ 5.5 μΩ·m |
| Bulk density | ≥ 1.60 g/cm³ | ≥ 1.65 g/cm³ | ≥ 1.70 g/cm³ |
| Flexural strength | ≥ 5.0 MPa | ≥ 6.0 MPa | ≥ 8.5 MPa |
| Typical relative performance | Standard conductivity and mechanical strength | Lower resistivity and higher strength than RP | Lowest resistivity and highest strength of the three grades |
| Typical application context | Commonly used in electric arc furnace steelmaking where operating conditions are less demanding | Used in more demanding furnace conditions and higher-current operation | Designed for very high-current, high-power electric arc furnace operation |
| Specification note: Values shown are representative grade-level reference limits, not guaranteed specifications for every 200 × 1,800 mm electrode. Actual limits and dimensional tolerances vary by applicable standard, production process, and purchase specification; confirm the current technical data sheet before procurement. | |||
For a 200 mm graphite electrode, roughly 6–10 kA can serve as an initial screening range for some EAF applications. It is not a universal rating. The allowable current depends on electrode grade, manufacturing quality, nipple connection, furnace practice, and cooling conditions. A 1,800 mm length does not determine the current capacity by itself.
Check the supplier’s technical data for maximum continuous current, bulk density, resistivity, and permitted current density. Then compare those figures with the furnace transformer, secondary circuit, and operating schedule.
During a heat, watch for connection heating, unusual oxidation, and uneven wear near the electrode tip. Small details matter. A rating that looks suitable on paper may not fit a furnace with frequent power changes.
For China-based manufacturers, request test data tied to the offered production batch, not only a general catalogue. Confirm whether the stated kA value is continuous or short-term, and ask how it was determined. Keep a cautious margin during commissioning, then review actual electrode consumption and joint temperatures. I would not rely on diameter alone; even a neat specification sheet can leave practical questions unanswered.
For buyers comparing Chinese manufacturers of 200 x 1,800 mm graphite electrodes, production capacity is more than a figure on a website. Ask how many machining lines handle this size and whether output is recorded by shift. A factory may report total electrode capacity, not capacity for your exact dimensions. Numbers need context. Request recent production schedules, inspection records, and sample measurements, including diameter, length, and tolerances.
Certifications can help assess quality systems, but check their scope, issuing body, and validity dates. Confirm that the covered site and product category match the supplier’s current operations. Export data adds another useful check: request redacted shipping records, destination regions, and shipment frequency. Compare these details with stated capacity and lead times. I would not treat one clean certificate as proof of consistent production; that assumption is easy to make and hard to verify remotely.
Tips: Ask for a live video tour of the machining and packing areas. Check electrode surface finish and end-face condition on samples. Verify test reports against batch numbers. If figures conflict, ask for clarification in writing. A small mismatch may have an ordinary explanation, but it still deserves a closer look.
For 200x1800mm graphite electrodes, compare suppliers against the same drawing and inspection method. Ask for permitted diameter and length deviations, plus checks for ovality and end-face condition. A single caliper reading can miss variation along the body. Request recent inspection records tied to production lots, not just a blank sample form. Small details matter.
Nipple fit deserves a separate check. Confirm thread dimensions, taper, and surface condition against the agreed specification. Ask whether thread gauges are used, and how damaged or out-of-tolerance pieces are handled. A clean-looking joint is not enough. Where practical, arrange a trial fit or review documented gauge results before shipment. Even a careful check may not predict every issue during furnace operation.
Lead time should include production, inspection, packing, and inland transport to the loading point. Ask for a realistic schedule and written notice of delays; unusually short promises deserve scrutiny. Quality records should identify the lot, test date, measured values, and corrective actions. Compare several orders if possible. A polished report can still leave gaps, so check that its figures match the supplied dimensions and acceptance criteria.
This site uses cookies. By continuing to browse the site, you are agreeing to our use of cookies.
OKLearn moreWe may request cookies to be set on your device. We use cookies to let us know when you visit our websites, how you interact with us, to enrich your user experience, and to customize your relationship with our website.
Click on the different category headings to find out more. You can also change some of your preferences. Note that blocking some types of cookies may impact your experience on our websites and the services we are able to offer.
These cookies are strictly necessary to provide you with services available through our website and to use some of its features.
Because these cookies are strictly necessary to deliver the website, refusing them will have impact how our site functions. You always can block or delete cookies by changing your browser settings and force blocking all cookies on this website. But this will always prompt you to accept/refuse cookies when revisiting our site.
We fully respect if you want to refuse cookies but to avoid asking you again and again kindly allow us to store a cookie for that. You are free to opt out any time or opt in for other cookies to get a better experience. If you refuse cookies we will remove all set cookies in our domain.
We provide you with a list of stored cookies on your computer in our domain so you can check what we stored. Due to security reasons we are not able to show or modify cookies from other domains. You can check these in your browser security settings.
We also use different external services like Google Webfonts, Google Maps, and external Video providers. Since these providers may collect personal data like your IP address we allow you to block them here. Please be aware that this might heavily reduce the functionality and appearance of our site. Changes will take effect once you reload the page.
Google Webfont Settings:
Google Map Settings:
Google reCaptcha Settings:
Vimeo and Youtube video embeds:
