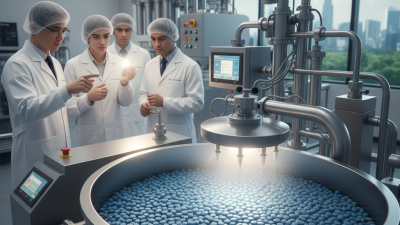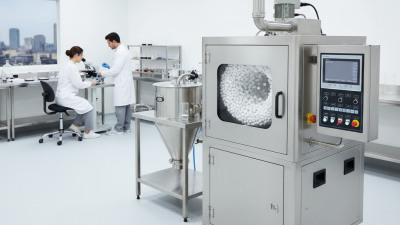
Selecting among top perforated pan coating machine manufacturers requires more than comparing catalog prices. A reliable machine must produce even coating, protect product quality, and support stable production over time. In practice, operators inspect spray coverage, pan rotation, drying control, cleaning access, and the accuracy of dosing systems. Small details matter. A poorly positioned spray nozzle can create uneven color, rough surfaces, or unnecessary material waste.
Experienced buyers also examine the manufacturer’s engineering record and service capability. Does the supplier provide process testing, installation guidance, spare parts, and responsive technical support? These questions reveal more than polished brochures. A trusted manufacturer should explain capacity limits clearly and provide documented performance data. Certifications, factory quality controls, customer references, and validation support can strengthen that assessment. Still, marketing claims deserve careful review.
Not every leading supplier suits every facility. Production scale, coating formulation, batch size, available floor space, and regional service access can change the final decision. A compact line may fit a growing plant better than a large automated system. That is worth considering. This guide compares top perforated pan coating machine manufacturers through practical factors, including equipment design, automation, hygiene, energy use, customization, and after-sales support. The evaluation is not perfect, because real performance depends on installation and operating conditions. Buyers should request trials and inspect finished samples before committing. A machine that looks impressive on paper may behave differently beside a busy production line. Reliable decisions come from evidence, careful questions, and realistic expectations.
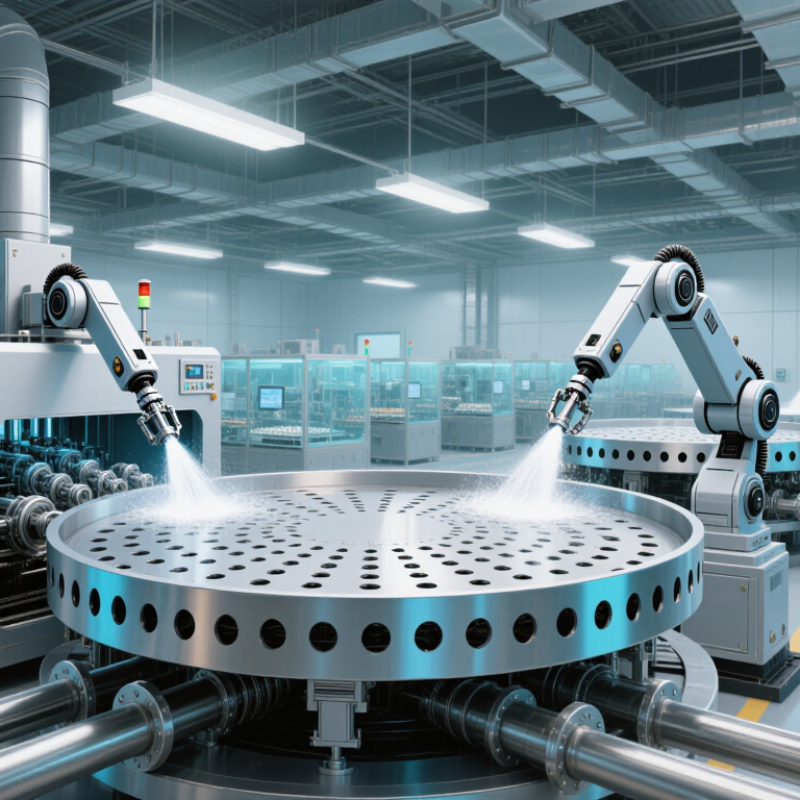
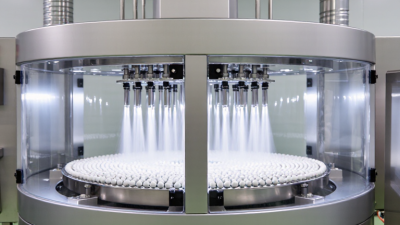
A perforated pan coating machine is industrial equipment used to coat tablets, pellets, or similar solid products. It uses a rotating perforated drum, spray guns, heated air, and an exhaust system. The perforations allow air to pass through the product bed. This improves drying and coating uniformity.
During operation, tablets tumble gently inside the pan while spray nozzles apply a controlled liquid layer. Heated air removes moisture through the drum, and exhaust airflow carries it away. Operators adjust pan speed, spray rate, inlet temperature, airflow, and atomizing pressure.
Excessive spray can create sticking, uneven color, or damaged tablet edges.
A reliable machine should provide stable airflow, accurate temperature control, easy cleaning, and smooth product contact surfaces. Stainless steel construction is common because it supports hygienic processing and routine inspection.
In practical production, nozzle alignment deserves close attention. A poorly positioned nozzle may leave dry zones, even when the control screen shows normal readings.
Some systems also include automatic recipe control and data recording, but automation cannot replace skilled monitoring. Operators still need to check tablet movement, surface appearance, and drying behavior.
I have found that performance specifications can look impressive on paper, yet cleaning access may remain inconvenient. That weakness deserves careful review before purchase.
A perforated pan coating machine rotates tablets inside a stainless-steel drum with thousands of small openings. As the pan turns, tablets cascade gently through a controlled spray zone. Nozzles apply a thin coating solution, while heated air moves through the tablet bed and exits through the perforations. This airflow removes solvent and helps form an even film.
The coating cycle is carefully balanced. Pan speed controls tablet movement. Spray rate affects surface wetting. Air temperature and volume govern drying. Too much heat can create rough surfaces. Too little airflow may cause sticking.
Small details matter.
A 2024 report by Grand View Research identifies solid-dose processing as a major pharmaceutical equipment segment, supported by stricter quality requirements and higher production efficiency targets. MarketsandMarkets also reports continued demand for automated coating systems, especially equipment with closed-loop monitoring and reduced material waste. These findings explain why modern machines increasingly use pressure sensors, exhaust monitoring, and automatic spray adjustment.
In practical operation, an operator first checks nozzle alignment and airflow balance. The machine then preheats the pan and loads the tablets. During spraying, sensors can track temperature, humidity, and pressure changes. In-process samples still matter. Automation reduces variation, but it does not eliminate judgment. A coating may look uniform while hiding weak adhesion or excess moisture. Manufacturers should validate drying time, spray distribution, and cleaning performance for each formulation. This is where experience remains difficult to replace.
A perforated pan coating machine rotates the tablet bed while heated, filtered air passes through the perforations. A spray system applies the coating solution evenly, and controlled airflow removes solvent or water to form a uniform film. The chart shows a representative aqueous film-coating profile using typical industrial operating temperatures.
When comparing top perforated pan coating machine manufacturers, examine how each system performs in real production conditions. Pan size and working volume should match your batch range, not just your largest order. A machine that runs well at full capacity may coat poorly with small loads. Ask manufacturers for trial data using your product, coating material, and target weight gain.
Spray technology deserves close attention. Compare nozzle layout, spray pressure control, atomization quality, and the distance between nozzles and tablet beds. Even coverage depends on more than nozzle quantity. Airflow is equally important. Look for adjustable inlet temperature, humidity control, exhaust balance, and clear airflow measurements. Small temperature changes can affect drying and surface appearance. They matter.
Automation features should support operators rather than confuse them. Evaluate recipe storage, touchscreen controls, alarm history, sensor accuracy, and batch reporting. Stainless steel construction, smooth welds, accessible filters, and tool-free cleaning reduce downtime. Ask whether the machine supports quick product changeovers. This detail is often underestimated. A complicated washdown process can erase impressive output figures.
Reliable manufacturers provide installation guidance, operator training, maintenance schedules, and responsive technical support. Request spare-parts availability and service response times in writing. Independent testing is useful, but it should include measurable results such as coating uniformity, process time, and energy use. Brochures can look precise while hiding practical limitations. A factory visit or witnessed trial may reveal vibration, overspray, or difficult cleaning points that specifications miss.
Top Perforated Pan Coating Machine Manufacturers
Top perforated pan coating machine manufacturers focus on controlled airflow, spray accuracy, and cleanability. These factors directly affect tablet appearance, weight gain, and release performance. A 2024 Grand View Research analysis estimates continued growth in pharmaceutical manufacturing equipment, driven by automation and stricter quality requirements. This trend supports demand for perforated pans with recipe control, closed processing, and improved data recording.
Experienced manufacturers usually offer machines with adjustable pan speed, variable inlet air temperature, and precise spray-gun movement. Operators should also examine nozzle access, washing validation, and batch-size flexibility. The International Society for Pharmaceutical Engineering emphasizes process understanding and documented control strategies. In practice, a beautiful machine can still fail if airflow changes across the bed. That detail is easy to miss. Some suppliers also provide factory acceptance testing, installation support, and operator training. These services can reduce commissioning errors, although results depend on the manufacturer’s technical team.
Tips: Compare coating uniformity data, not only drum capacity. Ask for test-batch records using your tablet shape and formulation. Check whether cleaning time is measured under realistic conditions. Review software audit trails and spare-part availability before purchase. A 2023 MarketsandMarkets report identifies automation as a major direction in pharmaceutical equipment development. Still, automation does not replace sound process knowledge. Smaller batches may need different spray rates, and standard settings may require adjustment.
Choosing a perforated pan coating machine manufacturer requires more than comparing prices. Grand View Research estimates the global pharmaceutical manufacturing equipment market will grow steadily through 2030, driven by automation and tighter quality expectations. That growth makes supplier capability especially important. Ask for documented coating results using your tablet size, coating suspension, and target weight gain. Generic demonstrations can mislead.
Check the manufacturer’s engineering depth. The machine should control pan speed, inlet air temperature, airflow, spray rate, and exhaust pressure consistently. Request batch records, alarm histories, and calibration procedures. ISPE guidance emphasizes process understanding, risk control, and reliable documentation during equipment qualification. A supplier should support FAT, SAT, installation qualification, and operational qualification. Do not accept vague promises. Written acceptance criteria matter.
Service capacity often separates a dependable manufacturer from an attractive seller. PMMI industry research continues to identify automation, digital monitoring, and lifecycle support as major equipment priorities. Confirm spare-part availability, remote diagnostics, operator training, and response times. Visit a reference installation if possible. Look closely at spray nozzles, seals, filters, and cleaning access. Small details matter. I would also test low-load and high-load conditions, not only the perfect production run. A polished trial may hide weaknesses. Reconsider any supplier that avoids difficult questions, changes specifications late, or cannot explain how coating uniformity is measured.
A practical, brand-neutral comparison framework for evaluating perforated pan coating machine manufacturers and technical proposals.
| Evaluation Dimension | Typical Industry Data or Requirement | What a Strong Manufacturer Proposal Should Include | Buyer Verification Method |
|---|---|---|---|
| Equipment Type | Perforated coating pans use a rotating perforated drum, process-air handling system, spray guns, exhaust filtration and control software. | Clear process-flow diagram showing air inlet, product bed, exhaust path, spray system, cleaning access and safety interlocks. | Review the general arrangement drawing and confirm that the airflow direction and spray-zone design match the intended product. |
| Batch Capacity | Pilot and production systems commonly range from approximately 5 kg to more than 1,000 kg per batch, depending on pan volume, fill level and product bulk density. | Working capacity stated separately from total pan volume, with minimum and maximum validated fill levels. | Request capacity calculations based on the actual tablet or multiparticulate bulk density and required operating fill ratio. |
| Pan Volume | Commercial systems may span roughly 10 L to over 2,000 L across development, pilot and production scales. | Usable volume, total volume, drum diameter, drum width and allowable operating speed clearly identified. | Check whether the proposed volume supports both current batches and planned future products without excessive under-filling. |
| Airflow Capacity | Typical installations may require several hundred to tens of thousands of m³/h, depending on pan size, product load and drying demand. | Airflow range, temperature range, humidity-control approach, pressure-drop assumptions and exhaust balance data. | Compare the stated airflow with product-specific drying studies and confirm that the HVAC system can supply the required air volume. |
| Spray System | Spray-gun quantity varies by pan size and coating rate; systems may use one gun for development work and multiple guns for production. | Gun type, nozzle size, spray-rate range, atomizing-air range, gun positioning, anti-drip design and recipe control. | Ask for a spray-rate map and verify that the system can maintain uniform coverage at the lowest and highest planned rates. |
| Coating Uniformity | Uniformity depends on pan speed, tablet-bed movement, spray pattern, inlet-air conditions, coating suspension properties and process time. | Documented development method using process-performance qualification, sample locations and acceptance criteria. | Require representative placebo or product trials and review weight gain, appearance, assay or thickness-uniformity results where applicable. |
| Pan Speed Control | Variable-speed drives are standard; the usable operating range must be matched to tablet size, friability and product load. | Speed range, acceleration control, torque monitoring and automatic recipe limits. | Confirm that the proposed speed range is supported by development data rather than relying only on the motor’s maximum speed. |
| Product Temperature Control | Temperature control is normally achieved through conditioned inlet air, exhaust control and product-temperature monitoring. | Validated sensor locations, temperature alarms, inlet-air control and independent high-temperature protection. | Check sensor calibration procedures and confirm that product temperature, not only inlet temperature, is monitored. |
| Containment and Dust Control | Containment requirements depend on the active ingredient, occupational exposure limit, powder characteristics and facility strategy. | Defined pressure cascade, sealed product-transfer points, exhaust filtration, dust-tight doors and containment test method. | Provide the manufacturer with the material hazard assessment and request a documented containment strategy before final design approval. |
| Cleaning and Changeover | Cleanability is influenced by drum access, spray-gun removal, product-contact geometry, drainability and cleaning-agent compatibility. | Product-contact parts made from suitable stainless steel, accessible internal surfaces, documented cleaning procedure and optional automated cleaning capability. | Inspect cleaning-access drawings and verify swab locations, drain points, residual-risk controls and expected changeover time. |
| Material and Surface Finish | Pharmaceutical product-contact areas commonly use stainless steel such as 316L; the required finish depends on the process and validation strategy. | Material certificates, weld-quality information, surface-finish specification and passivation or electropolishing details where required. | Specify product-contact materials and surface-finish requirements in the purchase specification and review certificates during inspection. |
| Automation and Data Integrity | Modern systems generally use PLC/HMI control with recipe management, alarms, trends and electronic batch records or exportable data. | User-access levels, audit trail, time-stamped records, backup and restore functions, recipe control and data-export format. | Request a live software demonstration and map each required data-integrity function to the user-requirement specification. |
| Regulatory Documentation | Pharmaceutical projects commonly require URS, functional specifications, design qualification, FAT, SAT, IQ, OQ and calibration records. | Complete validation-documentation package, traceability matrix, manuals, spare-parts list and documented change-control process. | Score the proposal by document completeness and confirm which documents are included in the quoted price. |
| Electrical and Area Classification | Electrical design must match the site voltage, frequency, local code and any classified-area requirements. | Electrical load list, panel drawings, component specifications, protection ratings and hazardous-area compliance where applicable. | Have the site electrical and EHS teams approve the design before manufacturing begins. |
| Safety Systems | Core safeguards normally include emergency stops, door interlocks, over-temperature protection, airflow alarms and motor protection. | Safety-risk assessment, interlock matrix, guarding details and clearly defined safe-state behavior. | Review the safety circuit during FAT and verify each alarm and interlock using an approved test protocol. |
| Scale-Up Capability | Successful scale-up requires comparable spray geometry, airflow distribution, pan motion, drying capacity and process-control philosophy. | Engineering scale data, similarity calculations and a documented transfer strategy from development to production equipment. | Ask for evidence from trials performed with a product or placebo having similar size, density, friability and coating requirements. |
| Service and Spare Parts | Availability of critical parts and qualified technical support directly affects uptime and validation continuity. | Response-time commitment, remote-support method, recommended two-year spare-parts list, training plan and preventive-maintenance schedule. | Evaluate local service coverage, technician qualifications and the lead time for critical components. |
| Total Cost of Ownership | Purchase price is only one element; utilities, filters, coating suspension losses, maintenance, cleaning time and downtime affect lifecycle cost. | Utility-consumption estimates, filter-replacement assumptions, maintenance intervals, warranty terms and optional-cost schedule. | Compare suppliers using a five- to ten-year lifecycle model rather than equipment price alone. |
| Recommended Selection Method | Technical complianceProcess trialsValidationService | Use a weighted scorecard with the highest weighting assigned to product quality, containment, cleanability, validation support and reliable service. | Shortlist only manufacturers that pass mandatory requirements, then compare documented performance, lifecycle cost and delivery risk. |
| Note: The numerical ranges above are broad screening values commonly encountered across development and production applications. Final equipment sizing must be confirmed through product-specific trials, engineering calculations, site-utility review and applicable regulatory requirements. | |||
This site uses cookies. By continuing to browse the site, you are agreeing to our use of cookies.
OKLearn moreWe may request cookies to be set on your device. We use cookies to let us know when you visit our websites, how you interact with us, to enrich your user experience, and to customize your relationship with our website.
Click on the different category headings to find out more. You can also change some of your preferences. Note that blocking some types of cookies may impact your experience on our websites and the services we are able to offer.
These cookies are strictly necessary to provide you with services available through our website and to use some of its features.
Because these cookies are strictly necessary to deliver the website, refusing them will have impact how our site functions. You always can block or delete cookies by changing your browser settings and force blocking all cookies on this website. But this will always prompt you to accept/refuse cookies when revisiting our site.
We fully respect if you want to refuse cookies but to avoid asking you again and again kindly allow us to store a cookie for that. You are free to opt out any time or opt in for other cookies to get a better experience. If you refuse cookies we will remove all set cookies in our domain.
We provide you with a list of stored cookies on your computer in our domain so you can check what we stored. Due to security reasons we are not able to show or modify cookies from other domains. You can check these in your browser security settings.
We also use different external services like Google Webfonts, Google Maps, and external Video providers. Since these providers may collect personal data like your IP address we allow you to block them here. Please be aware that this might heavily reduce the functionality and appearance of our site. Changes will take effect once you reload the page.
Google Webfont Settings:
Google Map Settings:
Google reCaptcha Settings:
Vimeo and Youtube video embeds: