Why Choose Different Types of Coating Machines?

Choosing among the different types of coating machine is a production decision, not a catalog decision. A roll coater may spread a smooth film across flexible packaging. A spray system may reach a complex metal surface more effectively. A curtain coater can deliver high speed, but it needs stable viscosity and careful web control.

Industry reports show why this choice matters. MarketsandMarkets’ Coating Equipment Market report identifies automation, transfer efficiency, and demand for consistent film thickness as major market drivers. Smithers’ report, The Future of Functional and Barrier Coatings to 2028, also highlights growing requirements for thinner, more precise protective layers. These findings point toward a practical truth: equipment must match the material, substrate, coating weight, line speed, and drying method.

Dr. Edward D. Cohen, a respected coating and drying technology specialist, has stated, “The coating process is a complex process involving many variables.” That sentence deserves attention. There is no universal machine. Not really. A laboratory dip coater may produce useful trial data, yet fail during continuous production. A high-speed slot-die system may reduce waste, but only when pump control and surface tension remain stable. Operators often learn this beside the line, watching a 0.2-millimeter streak become a costly reject.

The right types of coating machine should therefore be selected through trials, measurable specifications, and total operating costs. Energy use, cleaning time, maintenance access, and operator skill also matter. These details are easy to overlook. They should not be.
Why Choose Different Types of Coating Machines?

Coating Machines: Definition, Purpose, and Core Functions

Why Choose Different Types of Coating Machines?

Coating machines apply a controlled layer of liquid, powder, or film to a surface. Their core functions include metering, spreading, drying, curing, and inspection. In a production line, they turn uneven application into repeatable thickness, coverage, and finish. That choice matters.

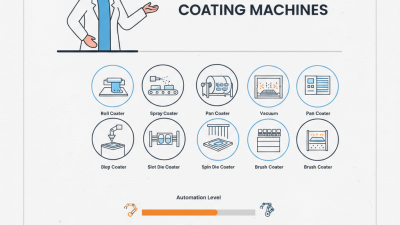
Different materials require different coating methods. Slot-die systems support precise, continuous layers, while roll coaters handle broad surfaces at high speed. Spray equipment suits complex shapes, but overspray can increase material waste. Dip systems cover three-dimensional parts effectively, although drainage and drying may be harder to control. The best machine depends on viscosity, substrate, line speed, coating weight, and the required tolerance.

Industry data shows why precision is becoming more important. Smithers’ 2024 assessment of the global flexible packaging market projects continued growth through 2029, increasing demand for reliable barrier and functional coatings. A MarketsandMarkets report also estimated the industrial coatings market could reach about 115 billion dollars by 2028, driven by infrastructure, transportation, and manufacturing applications. These figures indicate stronger pressure on equipment performance, not merely output volume.

In practice, operators monitor web tension, pump pressure, oven temperature, and surface energy. Small changes can create streaks, pinholes, or poor adhesion. No setup is perfect. An experienced technician still checks coated samples instead of trusting sensors alone. Some machines appear efficient but consume more energy during drying. Others deliver excellent precision but need slower speeds. Choosing different coating machines means matching real process conditions, not selecting the most complex equipment.

How Coating Machine Types Differ in Design and Operation

Coating machines differ because each design controls liquid, substrate, speed, and drying in a different way. A roll-to-roll machine guides flexible film through rotating rollers. It suits continuous production and steady coating thickness. Tension settings matter greatly. Too much tension can stretch the film and create uneven edges.

A blade or knife-over-roll machine spreads material across a moving sheet. Its gap setting directly affects wet thickness. Operators often inspect the coated surface under angled light. Small ridges, bubbles, or dry patches become easier to notice. Slot-die systems deliver coating through a narrow opening. They offer precise control, especially when material usage must remain low. However, the liquid must have suitable viscosity and flow behavior. A thick formulation may clog the die. A thin formulation may spread beyond the intended area.

Spray machines use pressurized nozzles and can cover complex shapes. Their design depends on droplet size, air movement, and nozzle distance. Dip coating is simpler, but withdrawal speed strongly affects the final layer. Faster withdrawal usually creates a thicker film. Drying units also separate machine types. Hot air, infrared energy, and controlled airflow produce different results. Temperature must match the substrate and coating chemistry. Excessive heat can warp film or damage sensitive surfaces. In practice, no machine design is perfect. A setup that performs well in testing may struggle during long production runs. Regular thickness checks and documented adjustments make operation more reliable.

Choosing a Coating Machine for Specific Materials and Products

Choosing a coating machine starts with the material, not the equipment catalogue. A water-based coating may need controlled drying and corrosion-resistant fluid paths. Solvent-based systems require sealed delivery, ventilation, and carefully rated components. Powder coatings demand electrostatic charging and recovery control. The product shape matters too. Flat panels suit roll coaters, while irregular metal parts often need spray or dip systems.

The market data supports this level of specialization. Grand View Research reported that the global paints and coatings market reached about USD 206.56 billion in 2023. Its forecast also indicates continued growth through 2030. MarketsandMarkets identifies powder coatings as a major technology segment, driven by industrial durability and reduced solvent use. These figures show why one machine rarely performs equally well across every application.

In practice, test viscosity, surface energy, heat sensitivity, and target film thickness before purchasing. A laboratory coater can reveal defects such as orange peel, pinholes, or uneven edges. Small details matter. For example, a thin film on aluminum may cure differently from the same film on engineered plastic. My experience suggests that throughput is often overvalued. A faster line can create more rejected parts when dosing is unstable. Selection is rarely perfect. Recheck the process after real production begins, because the first trial may hide seasonal humidity, operator variation, or material aging.

Key Factors for Comparing Coating Machine Performance

Choosing a coating machine depends on more than its advertised speed. The right comparison starts with the coating material, product width, and target thickness. A machine designed for liquid coatings may perform poorly with a high-viscosity formulation. I have seen this mismatch create uneven edges, clogged lines, and costly rework.

Performance should be measured with clear data. Check coating uniformity across the web, production speed, drying efficiency, and material waste. Record results at different speeds, not only under ideal conditions. Inspect samples under consistent lighting and measure thickness with calibrated equipment. Energy use also matters, especially when dryers operate for long shifts. Small temperature changes can affect solvent evaporation, surface appearance, and adhesion. These details often reveal more than a sales specification.

Maintenance and process control deserve equal attention. Compare cleaning time, roller adjustment, sensor accuracy, and access to replacement parts. A machine that runs quickly but requires frequent stoppages may reduce real output. Safety systems, operator training, and documented testing should also influence the decision. No comparison is perfect. My own evaluations have sometimes favored a slower machine because it produced fewer defects. That choice was not obvious at first. A trial using the actual coating, substrate, and operating conditions remains the most reliable test.

Why Choose Different Types of Coating Machines? - Key Factors for Comparing Coating Machine Performance

Coating Machine Type Typical Coating Thickness Typical Web Speed Coating Accuracy Suitable Viscosity Range Material Utilization Best-Suited Applications Main Performance Consideration
Slot-Die Coater Wet films from approximately 1 to 500 µm Approximately 5–150 m/min, depending on fluid and substrate Very high; excellent cross-web uniformity when properly adjusted Low to medium viscosity; formulation and die design are critical Very high; metered delivery produces little overspray or excess coating Battery electrodes, optical films, adhesives, separators and specialty coatings Requires precise pump control, die alignment, filtration and clean fluid handling
Gravure Coater Approximately 1–30 µm dry film, depending on cell volume and formulation Approximately 50–300 m/min High for repeatable patterned or uniform coating Low to medium viscosity, commonly solvent- or water-based inks and coatings High, although pan and circulation systems can create material losses Flexible packaging, decorative films, printed electronics and release liners Engraved-cylinder selection, doctor-blade condition and solvent management affect results
Reverse-Roll Coater Approximately 5–200 µm wet film Approximately 10–150 m/min High; supports smooth and uniform films over suitable substrates Low to high viscosity, depending on roll configuration and gap settings High to very high with a controlled coating pan or metering system Pressure-sensitive adhesives, films, foils, papers and functional coatings Roll speed ratio, nip pressure, web tension and air entrainment must be controlled
Knife-Over-Roll Coater Approximately 10–500 µm wet film Approximately 5–100 m/min Medium to high; strongly influenced by web flatness and coating rheology Medium to very high viscosity, including pastes and filled formulations High; excess material can normally be returned to the supply system Textiles, technical fabrics, heavy films, foils, papers and protective coatings Knife angle, gap, pressure and substrate compressibility determine coating weight
Curtain Coater Approximately 20–500 µm wet film Approximately 20–200 m/min High on smooth, stable substrates; less suitable for highly uneven webs Low to medium viscosity with good curtain stability High for continuous full-width coating; edge losses require management Paperboard, decorative panels, glass, films and other flat substrates Flow stability, curtain free-fall, substrate travel and edge control are essential
Spray Coater Approximately 10–300 µm wet film, depending on spray method Approximately 1–60 m/min for automated web or conveyor systems Medium; can be high with controlled robotic or electrostatic systems Low to medium viscosity; nozzle size and atomization affect performance Medium to low because overspray and booth recovery may be required Three-dimensional parts, irregular surfaces, metal components and protective finishes Atomization, booth ventilation, overspray recovery and operator or robot movement control
Dip Coater Approximately 10–1,000 µm wet film, depending on withdrawal speed and viscosity Approximately 0.1–20 m/min withdrawal speed Medium; thickness may vary with drainage, geometry and surface tension Low to high viscosity, provided drainage and drying are manageable High for complete immersion, although bath maintenance and drag-out create losses Complex-shaped components, corrosion protection, primers and laboratory development Withdrawal speed, bath contamination, drainage marks and drying behavior determine consistency

Note: Performance ranges are representative engineering guidelines rather than guaranteed machine specifications. Actual results depend on coating chemistry, solids content, substrate, web width, drying capacity, operating temperature and process control.

How Production Needs Determine the Best Coating Machine Type

Why Choose Different Types of Coating Machines?

How Production Needs Determine the Best Coating Machine Type

The right coating machine begins with the production target, not the machine catalog. A small batch operation may benefit from a flexible spray or dip system. It can handle frequent material changes and varied product sizes. For high-volume work, a roll or curtain coater may provide faster coverage and steadier output. Speed matters, but consistency matters more.

Material behavior also shapes the decision. Thick coatings may need controlled pressure and heated delivery lines. Low-viscosity liquids often require precise flow control and careful drying. The substrate adds another concern. Metal, film, wood, and formed parts respond differently to tension, heat, and contact. Experienced engineers usually test coating thickness, edge coverage, adhesion, and curing time before approving equipment.

Maintenance deserves equal attention. A machine that runs quickly but takes hours to clean may reduce real productivity. Operators should inspect access points, pump stability, nozzle wear, and control accuracy. Useful production records can reveal problems that demonstrations hide. No selection is perfect. A team may overestimate future capacity or underestimate cleaning work. That mistake is common. Small trials, measured results, and honest operator feedback create a more reliable choice. A machine should fit today’s process while allowing practical adjustments tomorrow.

Why Choose Different Types of Coating Machines?

How production needs determine the best coating machine type

How to read this chart: Roll-to-roll machines are generally suited to high-volume web production, while slot-die systems are preferred when coating thickness must be highly uniform. Spray and dip coating provide greater flexibility for complex three-dimensional parts, whereas curtain coating is effective for wide, flat surfaces requiring high throughput.

The scores represent general engineering suitability on a scale from 1 to 5. Actual machine selection should also consider coating viscosity, substrate shape, target thickness, drying capacity, material utilization, and required production speed.